Category Overview
External-axis welding systems integrate multi-axis articulated robot arms with synchronized external manipulators—such as headstock-tailstock positioners, linear sliders, and tilt-rotate tables. This configuration expands the effective work envelope, eliminates manual repositioning of heavy workpieces, and maintains continuous down-hand welding positions (1G/PA to 5G/PF). Built for high-duty-cycle industrial fabrication, multi-axis motion interpolation synchronizes robot torch trajectories with external workpiece manipulation to ensure stable heat input and precise seam tracking on oversized structures.
-
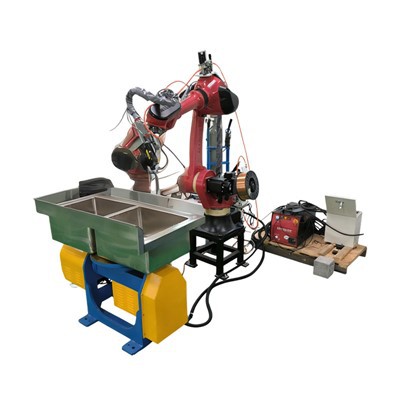
![Multi-Axis Welding Robot System]() Multi-Axis Welding Robot SystemThe Borunts Tech Multi-Axis Welding Robot System integrates a 6-axis articulated industrial robot with synchronized external axes—including dual-axis positioners and motorized floor tracks—to...
-
![Welding Robot With External Rotary Axis]() Welding Robot With External Rotary AxisThe BR-RA Series integrates a 6-axis industrial articulated robot with a synchronized external rotary axis (single-axis or dual-axis positioner). This configuration establishes coordinated...
-
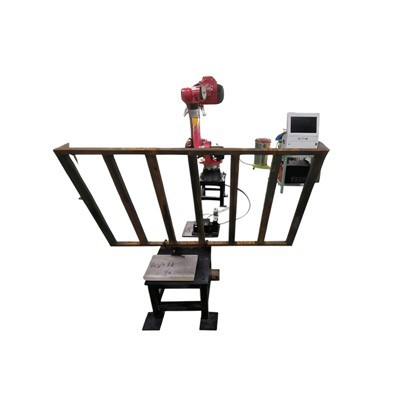
![Welding Robot With Overhead Linear Axis]() Welding Robot With Overhead Linear AxisThe Welding Robot with Overhead Linear Axis integrates a 6-axis articulated welding robot onto an overhead-mounted external linear track (7th/8th axis) in compliance with ISO 10218-1 and CE...
-
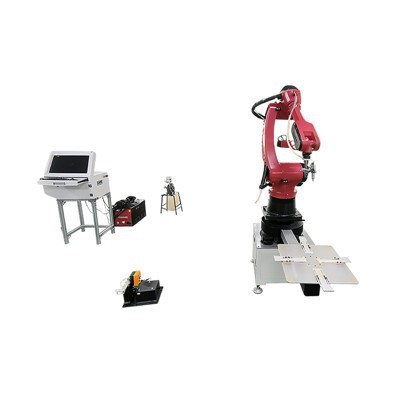
![Welding Robot With Floor-Mounted Linear Axis]() Welding Robot With Floor-Mounted Linear AxisThe Chuanglida Intelligent Equipment BRT-LA series integrates a 6-axis industrial welding robot with a precision-ground, floor-mounted linear slide rail. This 7-axis or 8-axis synchronized system...
-
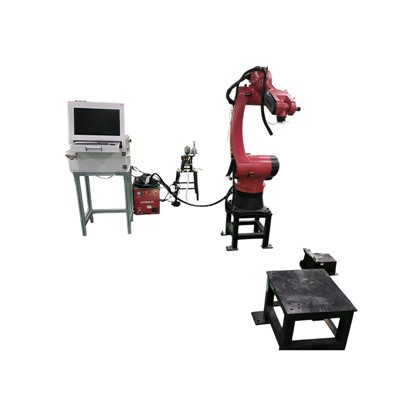
![Welding Robot With External Track Axis]() Welding Robot With External Track AxisThe Chuanglida Intelligent Equipment welding automation system integrates a 6-axis articulated industrial robot manipulator (such as the BRTIRWD1506A series, offering a 6 kg payload and 1647 mm...
-
![7-Axis Welding Robot]() 7-Axis Welding RobotThe Borunstech 7-Axis Welding Robot integrates a 6-axis articulated arm with a synchronized linear slide rail or coordinated workpiece positioner, backed by 15 years of cell deployments.


Product Range
Linear Track-Mounted Systems (7th Axis)
Extends robot longitudinal travel up to 15 meters via rack-and-pinion drives for long structural beams, trailer frames, and pipe racks.
Single-Axis Headstock-Tailstock Positioners
Engineered for cylindrical workpieces, shafts, and vessels with payload capacities from 500 kg to 5,000 kg.
L-Shaped Dual-Axis Tilt-Rotate Positioners
Enables 360-degree continuous rotation and +/-135-degree tilting for complex multi-plane weldments, keeping weld pools in the optimal flat position.
Gantry-Mounted Multi-Robot Cells
Integrates dual synchronized robots on overhead gantries with dual positioner stations for massive fabrications like construction machinery booms and bridge girders.
Technical Specifications
|
Technical Parameter |
Specification Value / Range |
|
Robot Payload Capacity |
6 kg to 210 kg |
|
External Axis Payload Capacity |
300 kg to 10,000 kg |
|
Robot Positional Repeatability |
±0.05 mm to ±0.08 mm |
|
External Axis Rotational Repeatability |
±0.05 deg |
|
External Axis Linear Repeatability |
±0.1 mm |
|
Synchronized Axes |
Up to 12 coordinated axes per master controller |
|
Maximum Positioner Rotation Speed |
1.5 rad/s to 3.0 rad/s |
|
Track Extension Range |
4 m to 30 m |
|
Modular Track Extension |
2 m increments |
|
Linear Robot Travel |
Up to 15 m |
|
Positioner Rotation |
360-degree continuous rotation |
|
Positioner Tilting Range |
±135 degrees |
|
Welding Processes |
GMAW (MIG/MAG), FCAW, GTAW (TIG), Plasma Arc, Laser-Hybrid |
|
Control Architecture |
Real-time industrial bus (EtherCAT, Profinet, Ethernet/IP) |
|
Welding Power Source Integration |
Digital and analog communication with major industrial welding power sources |
|
Positioner Configuration |
Headstock-Tailstock, Tilt-Rotate, Custom Fixture Positioners |
|
External Axis Configuration |
Linear Track, Rotary Axis, Tilt Axis, Multi-Axis Positioner |
|
Maximum Custom Positioner Capacity |
Up to 25 tons |
Key Features
Rigid Positioner Mechanical Structure
Fabricated from annealed structural steel weldments with precision-machined bearing housings to eliminate torsional deflection under eccentric loads up to 10 tons.
Integrated Thru-Hole Cabling & Swivel Joints
Pneumatic lines, shielding gas hoses, and motor power cables route through hollow-shaft positioner axes, preventing cable twisting during continuous rotation.
Collision Detection & Zone Monitoring
Software-based interference mapping and hardware limit switches protect against multi-axis collision in complex cell layouts.
Heavy-Duty IP67 Arm Protection
Wrist assemblies and joint seals withstand high-spatter environments and thermal radiation typical of continuous high-amperage structural welding.
Applications
Construction & Earthmoving Machinery: Excavator booms, loader frames, and bulldozer chassis requiring deep penetration welds on thick high-strength plates (Q345 / S355 / Hardox).
Commercial Vehicle & Trailer Manufacturing: Long longitudinal chassis rails, crossmembers, and axle housings utilizing linear track integration.
Pressure Vessels & Energy Equipment: Cylindrical tanks, wind turbine tower sections, and pipe spool fabrication requiring precise circumferential and longitudinal root-to-cap passes.
Rail Transportation: Bogie frames, structural underframes, and aluminum carbody components demanding strict dimensional tolerance and zero-defect weld integrity.
Vision-Guided Adaptive Seam Tracking: High-resolution laser profile scanners mounted adjacent to the torch provide real-time 3D joint tracking, automatically compensating for thermal distortion, part-to-part fit-up variations, and root gap fluctuations.
Through-The-Arc Seam Tracking (TATST): Voltage/current feedback monitoring for automatic torch path correction during heavy plate multi-pass welding.
Automatic Torch Cleaning Stations
Integrated reamers, wire cutters, and anti-spatter fluid sprayers to maintain contact tip cleanliness and stable arc ignition.
Pneumatic or Hydraulic Workpiece Clamping
Custom fixture jaws integrated into positioner faceplates for rapid, repeatable part loading and clamping pressure verification.
Fume Extraction Hoods & Enclosures
Retractable or fixed extraction ducts tied directly into cell safety interlocking circuits.
Customization
Tailored Kinematic Footprints
Custom rail lengths, gantry clear spans, and positioner span dimensions engineered to fit existing factory floor layouts and crane hook clearance limits.
Multi-Brand Controller Options
Integration with standard industrial controllers including FANUC, Yaskawa, ABB, and KUKA depending on plant maintenance standardization requirements.
Specialized Fixture Tooling
Design and fabrication of hydraulic/pneumatic clamping fixtures matched to specific customer CAD geometry and production takt times.
Safety Cell Partitioning
Perimeter fencing, light curtains, area scanners, and safety PLC programming configured to OSHA (North America) or CE EN ISO 10218 / ISO 13849-1 (Europe) standards.
Manufacturing & Quality Control
Plate Cutting & Preparation: CNC fiber laser and heavy plasma cutting machines process raw structural plates; edge beveling is performed via automatic milling to ensure root opening accuracy.
Weldment Stress Relief: All structural frames for robots, tracks, and positioners undergo thermal annealing in stress-relieving furnaces prior to final precision machining to prevent geometric warping over time.
CNC Machining Centers: Base plates, gearbox mounting faces, and positioner trunnions are machined on large-format CNC floor borers holding positional tolerances within 0.015 mm.
Load & Accuracy Testing:
Positioners undergo 120 percent rated payload static testing and 100 percent rated dynamic endurance cycling for 72 continuous hours.
Laser interferometer testing verifies linear track positioning accuracy and repeatability.
Harmonic drive backlash and gearbox clearance measurements are recorded prior to assembly sign-off.
Standards & Safety
CE Compliance
Conforms to European Machinery Directive 2006/42/EC, Low Voltage Directive 2014/35/EU, and EMC Directive 2014/30/EU.
Safety Standards
Engineered in accordance with ISO 10218-1/2 (Robots and robotic devices - Safety requirements) and ISO 13849-1 (Safety-related parts of control systems, Performance Level d/e, Category 3).
Electrical Compliance
Control cabinets built to NFPA 79 (North America) or IEC 60204-1 (Europe) standards with UL/CSA or TÜV-certified electrical components.

Why Choose Us
In-House Heavy Machining Capability: Full production control from raw steel plate cutting and thermal stress relief to 5-axis CNC machining of positioner gearboxes, eliminating third-party machining bottlenecks.
Rigorous Factory Acceptance Testing (FAT): Every integrated cell is fully assembled, dry-run tested, and calibration-verified on our test floor before crating, complete with certified laser test reports.
Direct Engineering Support: Access to experienced automation application engineers who review customer CAD data, perform cycle-time simulations, and provide complete kinematic layout proposals.
Robust Export Packaging: Vacuum-sealed moisture barrier bags, desiccants, and ISPM 15 heat-treated wooden crates protect sensitive electronics and precision-machined surfaces during transit.
FAQ
As one of the most professional external-axis welding robots manufacturers and suppliers in China, we also support customized service. Please feel free to buy discount external-axis welding robots in stock here from our factory. For price consultation, contact us.
Heavy Duty MIG Welding Workstation, robot laser welding machine, welding robot industrial production cell