
Industrial Automation & Fabrication
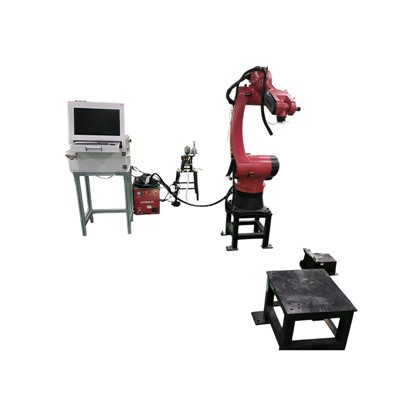
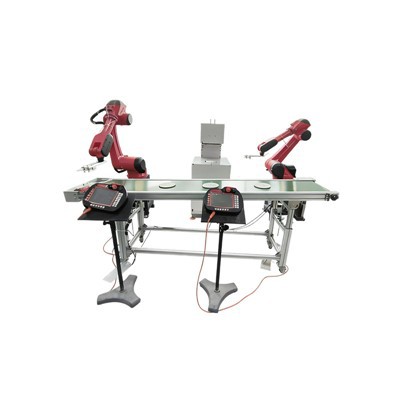
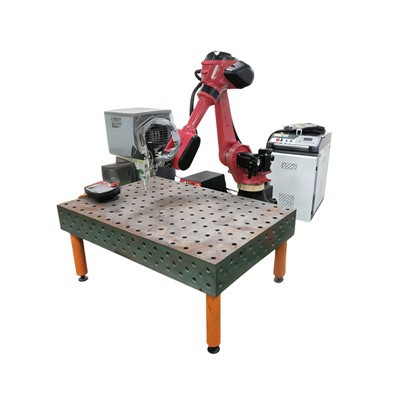
The Borunstech Flexible MIG Welding System is engineered for automated and semi-automated production lines requiring precise arc control across complex joint geometries. Its modular architecture decouples the wire-feed mechanism, power source, and multi-axis positioning arm to reduce torch-tip inertia, minimizing vibration during high-speed directional changes to maintain consistent bead profile tolerances on carbon steel, stainless steel, and aluminum alloys.
System Architecture:
IGBT-based Multi-Process Power Inverter
Precision Push-Pull Wire Feed Unit
Articulated Flex-Arm / Robotic Interface
Digital Control Panel & PLC Fieldbus Module
Key Features
Dual-Drive Push-Pull Wire Feed Mechanism: Prevents bird-nesting and wire deformation over umbilical lengths up to 10 meters, holding wire delivery speed within +/- 1% tolerance.
Real-Time Synergistic Waveform Control: Automatically correlates voltage and current with wire feed speed feedback to suppress spatter during short-circuit and pulse MIG transfers.
Modular Umbilical Routing: Encapsulates copper power cables, shielding gas lines, and control signals inside a wear-resistant, high-flex polyurethane sheath rated for 5 million bending cycles.
Open-Architecture PLC Interface: Integrates directly with third-party industrial robots and gantry systems via Profinet, EtherNet/IP, and Modbus TCP.
Closed-Loop Liquid Cooling: Employs a high-displacement brass pump and stainless steel radiator to keep torch body temperatures below 50 deg C at 100% duty cycle.
Technical Specifications
|
Parameter |
Specification Value |
|
Primary Input Voltage |
380V +/- 10%, 3Ph, 50/60Hz |
|
Rated Output Current |
400A (500A optional variant) |
|
Duty Cycle (40 deg C ambient) |
100% at 350A; 60% at 400A |
|
Wire Diameter Compatibility |
0.8 mm - 1.6 mm (Solid / Flux-cored) |
|
Wire Feed Speed Range |
1.5 m/min - 22 m/min |
|
Shielding Gas Compatibility |
Ar, CO2, Ar/CO2 mixtures (Mass flow controlled) |
|
Communication Protocols |
EtherNet/IP, Profinet, DeviceNet, RS485 |
|
Enclosure Protection Class |
IP23 (Power source), IP54 (Wire feeder) |
Applications
Automotive Sub-Frame Assembly: Continuous seam welding of high-strength low-alloy (HSLA) chassis components with strict penetration depth control, achieving an average single-shift productivity increase of 30% in automated Tier-1 lines.
Heavy Machinery Fabrication: Multi-pass fillet welding on thick-section structural excavator booms and crane masts under heavy structural load requirements.
Pressure Vessel Manufacturing: Circumferential and longitudinal mechanized welding of stainless steel tanks under ASME Section IX welding procedure specifications (WPS).
Railway Rolling Stock: Joining large aluminum structural extrusions for high-speed train car bodies using pulse MIG modes to control heat input and limit thermal distortion.
System Modules
Power Source: Inverter utilizing fourth-generation IGBT modules with a 45 kHz switching frequency for rapid transient response.
Wire Feeder: Forged aluminum four-wheel drive assembly featuring tool-less drive roll replacement and digital encoder feedback.
Flex-Torch Assembly: Air-cooled or water-cooled motorized torches with interchangeable neck angles (22 deg, 45 deg, 180 deg) for restricted joint access.
Control Pendant / HMI: 7-inch industrial touchscreen interface for parameter storage, error logging, and real-time current/voltage waveform monitoring.
Customization Options
Extended Umbilicals: Cable harness lengths from 3m to 15m for large-envelope gantry setups.
Specialized Torch Geometries: Low-profile torch necks designed for confined box-section weldments.
Multi-Torch Synchronization: Dual-head configurations driven by a single master PLC for simultaneous symmetrical welding.
Custom Software Profiles: Tailored pulse waveform libraries pre-calibrated for proprietary alloy compositions.
Manufacturing & Quality Control
Cabinet Fabrication: CNC fiber laser cutting and 250-ton hydraulic press brake bending ensure rigid, distortion-free enclosures.
PCB Assembly: Surface Mount Technology (SMT) lines equipped with Automated Optical Inspection (AOI) for all inverter control boards.
Winding Department: Automatic copper transformer winding and vacuum pressure impregnation (VPI) with Class H insulating varnish to withstand continuous thermal stress.
Factory Testing & Compliance: Every power source undergoes a 4-hour full-load burn-in test at 50 deg C, high-voltage dielectric strength testing (2000V for 1 minute), and arc simulation prior to crating. Manufactured under ISO 9001 frameworks, with CE conformity declarations and ASME-compliant material test reports (MTR) provided.
Lifecycle Support & Maintenance Assurance
Spare Parts Availability
Critical wear items (contact tips, gas diffusers, drive rolls, liner assemblies) stocked in regional hubs with guaranteed 48-hour dispatch.
Remote Diagnostics
Secure industrial gateway access for remote parameter tuning and firmware updates.
Preventive Maintenance Schedule
Daily: Inspect contact tips, clean wire feed drive rolls, check shielding gas flow rates.
Monthly: Inspect power cable insulation, clear internal cooling radiator fins with compressed air, calibrate wire feed speed encoder.
Annually: Perform insulation resistance testing on main transformer windings and verify output current calibration against certified shunt meters.
FAQ
Q: Can this system integrate with third-party articulated robots such as KUKA or FANUC?
A: Yes. Standard digital/analog I/O alongside industrial fieldbus cards (Profinet/EtherNet/IP) enable direct command execution from any major robot controller.
Q: What is the maximum recommended distance between the wire feeder and the welding torch?
A: The push-pull configuration supports a maximum separation distance of 8 meters without wire slippage or arc instability.
Q: Does the system support synergic parameter adjustment for aluminum welding?
A: Yes. The onboard micro-controller includes pre-installed synergistic curves for 4000 and 5000 series aluminum alloys during pulse MIG operation.
Q: What documentation is supplied with each shipment?
A: English technical manuals, electrical schematics, component bills of materials (BOM), factory calibration certificates, CE conformity declarations, and structural MTRs.
Hot Tags: flexible mig welding system, China flexible mig welding system manufacturers, suppliers, factory, 3d robot fiber laser cutting machine, cobot robot welding cobot, robot laser welding machine, robotic laser cutting machine, robotic welding structural steel system, welding robot industrial production cell