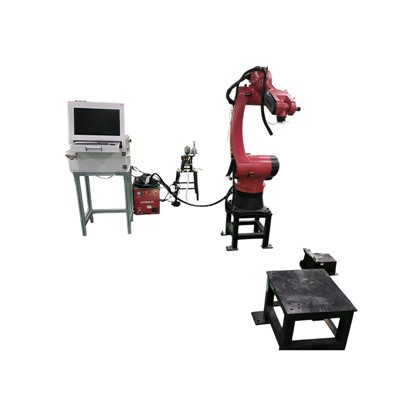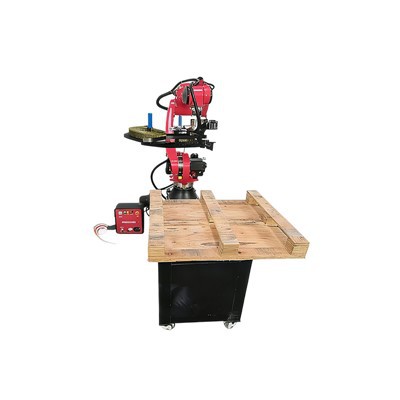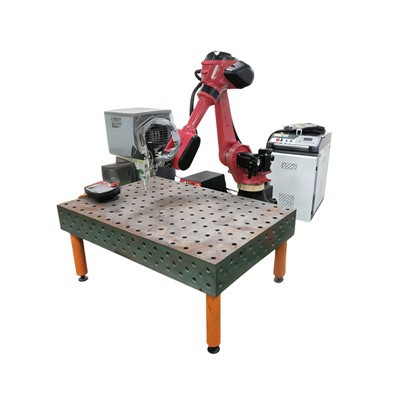

The Borunts Tech Floor-Mounted Rail Welding Robot integrates an articulated industrial robot onto a precision-machined ground linear track, expanding the operational envelope for large-scale structural welding. Engineered for heavy fabrication, the system synchronizes multi-axis motion--combining arm articulation with linear travel--to execute continuous welds on workpieces exceeding standard robotic reach.
Constructed with a heavy-wall structural steel base and a ground helical rack-and-pinion drive, the gantry-free ground track layout maintains rigidity under high payloads while preserving overhead crane access for loading and unloading.
Key Features
Rigid Ground Track Base: Fabricated from structural steel profiles, stress-relieved post-machining to prevent thermal or mechanical deformation over extended travel.
Synchronized Multi-Axis Motion: Integrates external track axes directly into robot controller kinematics for interpolated movement between linear travel and torch manipulation.
Heavy-Duty Linear Guideways: Uses heavy-load roller bearing blocks and induction-hardened rail profiles to support dynamic payloads up to 200 kg without deflection.
Enclosed Cable Management: Heavy-duty dynamic energy chain routes welding power cables, shielding gas lines, and control signals, protected from weld spatter.
Modular Track Extension: Bolted track segments allow field expansion in 2-meter increments, accommodating workpieces from 6 meters to 30+ meters.
Sealed Drive Architecture: Servo-driven gearboxes equipped with multi-lip seals and positive air purge ports prevent metallic dust and spatter ingress.
Technical Specifications
|
Technical Parameter |
Specification Standard |
|
Available Track Length |
6,000 mm to 30,000 mm (Modular 2m increments) |
|
Linear Travel Speed |
Up to 1.5 m/s (Configurable via servo tuning) |
|
Positional Repeatability |
+/- 0.05 mm along linear axis |
|
Compatible Robot Payloads |
100 kg, 120 kg, 165 kg, 210 kg |
|
Drive Mechanism |
Precision ground helical rack and low-backlash planetary gearbox |
|
Lubrication System |
Automatic progressive grease lubrication for rack and guide blocks |
|
Compatible Robot Brands |
Fanuc, Yaskawa, ABB, KUKA (Standard industrial controllers) |
|
Welding Power Source Interface |
Analog, DeviceNet, EtherNet/IP, Profinet (Fronius, Miller, Lincoln, EWM) |
|
Operating Environment |
0 deg C to 45 deg C, relative humidity <95% non-condensing |
Applications
Railcar & Locomotive Manufacturing: Continuous welding of long structural underframes, side sills, and bolster assemblies.
Construction & Mining Machinery: Longitudinal and circumferential welding of excavator booms, crane girders, and heavy chassis frames.
Steel Structure Fabrication: Automatic multi-pass welding of large box columns, H-beams, and bridge structural components.
Shipbuilding: Assembly and welding of long web frames, stiffeners, and deck panel sub-assemblies.
Pressure Vessel & Tank Production: Longitudinal seam welding for large cylindrical storage tanks and industrial boilers.
Welding System Integration
Motion Control: The robot controller acts as the master, managing synchronized interpolation between the robot arm and the rail axis via dedicated servo drives and absolute encoders.
Process Equipment: Accommodates MIG/MAG (GMAW), Pulsed MIG, Tandem MIG, and Flux-Cored Arc Welding (FCAW). Wire feed units mount directly to the robot arm or saddle carriage to minimize wire feeding resistance.
Seam Tracking: Compatible with laser vision seam trackers for real-time joint tracking and adaptive multi-pass filling on thick plates.
Torch Maintenance: Integrated automatic torch cleaner and wire cutter station positioned at the rail home position to execute programmed cleaning cycles.
Customization Options
Track Configuration: Custom stroke lengths tailored to factory floor layouts, including floor-flush embedding or raised foundation mounting.
Tandem Setup: Dual robot arms operating independently or synchronously on a shared rail system to double productivity.
Integrated Workholding: Synchronized headstock-tailstock positioners or roller beds mechanically linked and controlled alongside the rail axis for 360-degree manipulation.
Environmental Protection: Heat shields, water-cooled torches, and stainless steel telescopic covers for high-temperature or heavy-spatter environments.
Safety Systems: Light curtains, safety PLC integration, perimeter fencing, and pneumatic sliding access gates compliant with ISO 10218.
Manufacturing, Quality Control & Regulatory Compliance
Material Verification: Structural track components utilize carbon steel (ASTM A572 Grade 50 / Q355B equivalent), verified via mill test certificates prior to machining.
Precision Machining: Linear rail mounting surfaces and rack mating faces are ground on CNC floor boring and milling machines to guarantee straightness within 0.05 mm per 3 meters.
Heat Treatment: Base frames undergo post-weld thermal stress relief annealing in a gas-fired furnace to eliminate residual internal stresses.
Dimensional Inspection: Every rail section and carriage assembly is inspected using laser interferometers and electronic levelers to verify straightness, parallelism, and pitch accuracy.
Factory Acceptance Testing (FAT): Fully assembled systems undergo a 72-hour continuous dry-run test load cycle at rated speed prior to export.
Compliance Standards: Manufactured under an ISO 9001 quality management system. Electrical and mechanical subsystems comply with CE directives and ISO 10218 (Industrial Robot Safety Requirements).
Lifecycle Support & Maintenance Assurance
Installation & Commissioning: On-site mechanical alignment, laser calibration electrical integration, and joint-programming support executed by field service engineers.
Spare Parts Availability: Critical wear items--including drive pinions, gearboxes, cable chains, and guide bearing blocks--maintained in stock for immediate dispatch.
Remote Diagnostics: Secure remote access modules integrated into the control cabinet for real-time error logging, software updates, and parameter adjustments.
Preventative Maintenance: Technical documentation detailing daily inspection points, lubrication intervals, and backup battery replacement schedules.
FAQ
Q: What is the maximum single-piece travel length available?
A: Standard modular track segments allow continuous travel lengths up to 30 meters. For applications exceeding 30 meters, custom structural foundation designs and multi-segment splicing alignment fixtures are implemented.
Q: Can this rail system integrate with existing legacy welding robots?
A: Yes. The linear track can be supplied as a standalone 7th-axis kinematic unit with an independent servo drive and PLC interface, or fully integrated into major robot controller architectures (Fanuc, Yaskawa, ABB, KUKA).
Q: How is the linear rail protected from heavy welding spatter?
A: The system includes telescopic steel covers or flexible bellows over the guide paths, alongside scraper seals on the bearing blocks to clear debris during travel.
Q: What foundation requirements are necessary for installation?
A: A reinforced concrete floor with a minimum thickness of 250 mm to 300 mm is required. Precision leveling plates and chemical anchor bolts (or cast-in anchor plates) are supplied to maintain track alignment under dynamic load.
Hot Tags: floor-mounted rail welding robot, China floor-mounted rail welding robot manufacturers, suppliers, factory, Automated Welding Robots, automatic pneumatic welding robot, industrial welding automation cell, laser robot, robotic spot welding machine, robotic welder