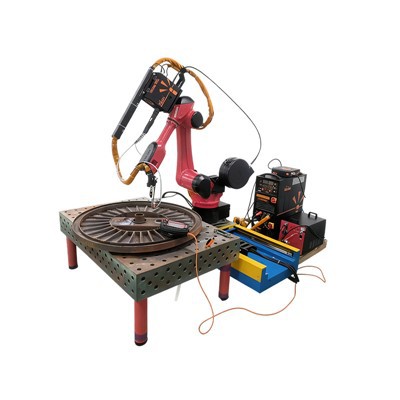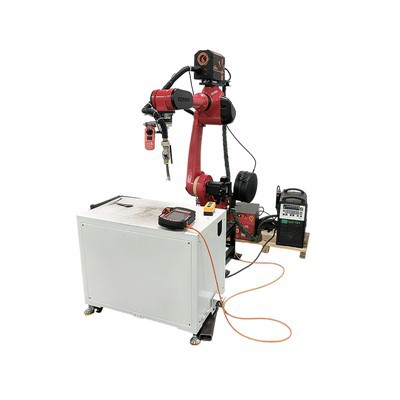

The Borunts Tech Flexible Robotic Welding Cell is a pre-configured, skid-mounted automated welding system for structural carbon steel, stainless steel, and aluminum components. Built on a stress-relieved structural steel base, it integrates a 6-axis industrial robot, dual-station servo positioners, a synergic welding power source, and an ANSI/RIA-compliant safety enclosure. Shipped as a pre-aligned, pre-wired single unit, it eliminates field installation alignment errors and accelerates cycle times for high-mix production runs.
Key Specifications & Performance Parameters
|
Parameter |
Specification Details |
|
Robot Payloads & Brands |
6 kg - 50 kg (FANUC, Yaskawa, ABB, KUKA) |
|
Robot Repeatability |
±0.03 mm to ±0.06 mm |
|
Positioner Capacity |
500 kg - 2000 kg per station (H-Frame / Ferris-Wheel) |
|
Welding Power Sources |
Lincoln Electric, Fronius, Miller (350 A to 500 A, 100% duty cycle) |
|
Non-Arc Time (Dual Station) |
< 3 seconds via pneumatic/servo safety partition |
|
Seam Tracking & Compensation |
Touch sensing & Through-The-Arc Seam Tracking (TAST) for gaps up to 3 mm |
|
Torch Collision Protection |
Mechanical clutch with optical break-detection (12 ms emergency stop) |
|
Electrical & Utility Supply |
380V - 480V ± 10%, 3-Phase, 50/60 Hz; Dual-zone digital gas mass flow control |
|
Standard Footprint (L x W x H) |
4200 mm x 2400 mm x 2600 mm (Scalable to fixture size) |
|
System Weight |
3200 kg - 5500 kg |
Industrial Applications
Automotive Sub-Assemblies: Cross-members, seat frames, and suspension control arms using high-strength low-alloy (HSLA) steel.
Heavy Machinery: Hydraulic cylinder brackets and structural cabin frames utilizing thick-plate carbon steel up to 25 mm.
Enclosures & HVAC: Stainless steel junction boxes and air-handling frames requiring spatter-free TIG or pulsed MIG welding.
System Architecture & Integration
Mechanical Datum: Robot pedestals and positioner tooling sub-bases are machined from a single weldment, maintaining a 0.05 mm relative mechanical tolerance.
Control & Communication: EtherNet/IP and Profinet protocols link the robot controller, welding power source, and PLC. The HMI stores up to 255 unique part programs with OPC UA data export.
Maintenance Automation: Pneumatic torch cleaner station with automated reamer, anti-spatter fluid sprayer, and wire cutter operating on programmable cycle counts.
Safety Architecture: Heavy-gauge sheet steel base plates with polycarbonate/wire-mesh upper panels interlocked via dual-channel safety switches conforming to ISO 13849-1 (Cat 3, PL d/e) and ISO 10218-1/2.
Engineering Customization
Fixture Tooling: Quick-change hydraulic or pneumatic clamping sub-plates engineered from customer-supplied 3D CAD data.
Vision Guidance: 2D or 3D laser scanners mounted to the torch assembly for joint tracking on high-variance geometries.
Process Adaptability: Multi-purpose cell layout capable of quick changeovers between MIG welding, plasma cutting, or stud welding.
Manufacturing & Quality Control
Machining & Stress Relief: Base frames and positioner trunnions are milled on CNC floor borers following thermal annealing and vibrational stress relief.
Electrical Compliance: Control panels are built in an ISO-compliant facility using numerical terminal labeling and wire ferrules meeting UL508A and NFPA 79 standards.
Factory Acceptance Testing (FAT): Mandatory 72-hour burn-in execution utilizing customer material coupons, verified via CMM dimensional checks prior to crating.
Lifecycle Support & Logistics
Pre-Shipment Documentation: Layout drawings, foundation loading diagrams, and utility schematics issued 4 weeks prior to dispatch.
Deployment & Training: Factory deployment engineers handle mechanical anchoring, utility hookup, and a 5-day on-site operator/programmer training program.
Remote Diagnostics: Secure onboard VPN router integrated into the PLC cabinet for remote ladder logic and error log troubleshooting.
Spare Parts Inventory: Critical wear components (contact tips, gas nozzles, swan necks, drive rolls) stocked for same-day dispatch.
FAQ
Q: What is the standard lead time and installation duration?
A: Shipment takes 8 to 10 weeks from order finalization. On-site installation, integration check, and production sign-off require 5 to 7 working days, assuming facility utilities are routed to the cell perimeter.
Q: How are changeovers handled for multi-variant production?
A: Operators select active recipes via the HMI touchscreen, while pneumatic quick-change fixture sub-plates locate via tapered pins, allowing manual changeovers in under 10 minutes.
Q: What welding wires and shielding gases are supported?
A: The standard configuration supports solid or flux-cored wires from 0.8 mm to 1.6 mm diameter, utilizing Argon/CO2 mixtures for carbon steel and pure Argon for stainless steel and aluminum.
Hot Tags: flexible robotic welding cell, China flexible robotic welding cell manufacturers, suppliers, factory, 20kg Heavy-Duty Welding Robot, automated welding fixture handling system, Automated Welding Robots, robotic welding arm, tig welding robot system, welding robot arc control system