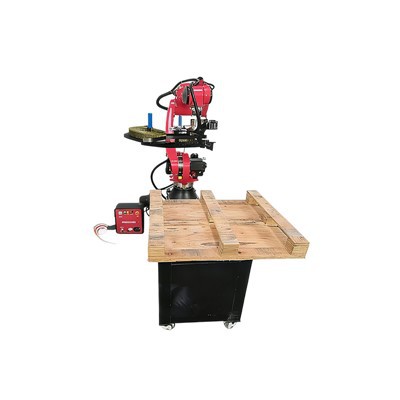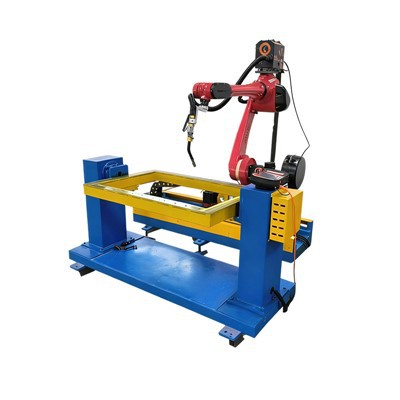

The Chuanglida Intelligent Equipment Gantry Welding Robot is engineered for structural fabrication of oversized components that exceed articulated arm reach. Built on a stress-relieved steel box-section gantry, the system ensures stable multi-axis motion across expansive workspaces. It supports high-deposition processes-Submerged Arc Welding (SAW) and Gas Metal Arc Welding (GMAW)-maintaining consistent torch placement across extended travel lengths without harmonic vibration.
Key Features
Dual-Drive Gantry Structure: Synchronized AC servo drives on the X-axis bridge prevent mechanical skewing across spans up to 12 meters.
Modular Axis Architecture: Scalable from 3 core axes (X, Y, Z) to 7 synchronized axes by incorporating motorized cross-slides, external positioners, and rail carriages.
Adaptive Seam Tracking: Real-time laser or arc-sensing feedback corrects for thermal distortion and joint fit-up variations during multi-pass thick-plate welding.
Heavy-Payload Z-Axis Ram: Counterbalanced vertical ram supports welding heads and wire feed mechanisms up to 50 kg payload without mechanical backlash.
Technical Specifications
|
Technical Parameter |
Standard Specification Range |
Customization Limits |
|
X-Axis Travel (Bridge Span) |
4,000 mm - 12,000 mm |
Up to 24,000 mm via modular track extensions |
|
Y-Axis Travel (Carriage Stroke) |
2,000 mm - 4,500 mm |
Scalable to application clearance requirements |
|
Z-Axis Travel (Vertical Stroke) |
1,000 mm - 2,500 mm |
Telescopic ram options available |
|
Linear Positioning Accuracy |
plus-minus 0.1 mm / 1000 mm |
Laser-calibrated compensation mapping |
|
Repeatability |
plus-minus 0.05 mm |
Closed-loop encoder feedback |
|
Maximum Traverse Speed |
15,000 mm/min (X/Y axis) |
Programmable acceleration profiles |
|
Compatible Processes |
GMAW, FCAW, SAW, Tandem MIG |
Dual-wire configurations supported |
|
Control System |
Industrial CNC / Multi-axis PLC |
Siemens Sinumerik / Beckhoff architecture |
Applications
Pressure Vessels & Boilers: Longitudinal and circumferential seams for cylindrical shells up to 6 meters in diameter and 50 mm wall thickness.
Construction & Mining Equipment: Excavator booms, crane jibs, and heavy chassis frames requiring deep-penetration multi-pass fillets.
Wind Energy Infrastructure: Tower section fabrication and internal ring flange welding.
Bridge & Structural Steel: Box girder fabrication, orthotropic deck panels, and heavy H-beam stiffener attachment.
Welding System
Process Adaptability: Supports single-wire, twin-wire, and tandem SAW configurations for deposition rates exceeding 15 kg/h.
Wire Feed Management: Dual-motor push-pull units prevent bird-nesting over umbilical lengths up to 15 meters.
Flux Recovery Unit: Continuous pneumatic recovery system recycles unused flux back to the hopper during SAW operation.
Fume Extraction Integration: Gantry-mounted extraction hoods routed to filtration units via articulated ducting.
Customization Options
Footprint Engineering
Floor-mounted rails, overhead gantry suspensions, or portable transport bases.
Workpiece Interfacing
Synchronization protocols for turning rolls, hydraulic positioners, and head-tailstocks up to 50-ton capacity.
Vision & Sensing
Custom laser profile scanners for root gap measurement and adaptive fill pass generation.
Environmental Hardening
Heat shields, water-cooled torches, and dust-sealed gearboxes for harsh plate-shop environments.
Manufacturing & Quality Control
Structural Annealing: All weldments undergo full thermal stress relief annealing in a 15-ton gas-fired furnace prior to precision CNC machining to eliminate residual stresses and prevent warping.
Precision Machining: Gantry rails and mating surfaces are machined on large-format CNC floor borers in temperature-controlled metrology rooms to maintain straightness tolerances within 0.05 mm per meter.
Dimensional Verification: Laser tracker verification reports are generated for every gantry system prior to factory tear-down.
Electrical Compliance: Control panels adhere to UL508A / NFPA 79 standards or CE/IEC 60204-1 directives using industrial shielded cabling and redundant safety interlocks.
Lifecycle Support & Maintenance Assurance
Remote Diagnostics: Secure VPN module integrated into the CNC controller for remote firmware updates, I/O monitoring, and collaborative troubleshooting.
Preventive Maintenance: Documented wear-part replacement schedules for drive belts, contact tips, wire feed rollers, and linear guide wipers.
Spare Parts Inventory: Critical motion components (servo motors, drives, gearboxes, sensors) stocked locally for dispatch within 48 hours.
On-Site Commissioning: Factory-certified service technicians supervise mechanical assembly, laser alignment, path calibration, and initial production run-offs.
FAQ
Q: How does the gantry system compensate for thermal deflection during continuous high-amperage SAW welding?
A: Structural beams utilize heavy-gauge steel tubes with internal ribbed baffling to minimize torsional twist. The CNC controller also applies real-time thermal drift correction algorithms based on embedded pyrometer feedback where required.
Q: Can this gantry system integrate with our existing roller beds and positioners?
A: Yes. Open-standard fieldbus communication (ProfiNet, EtherCAT, Ethernet/IP) enables handshaking signals and speed synchronization with third-party turning rolls and hydraulic positioners.
Q: What is the typical installation and commissioning timeframe?
A: Standard installation requires 7 to 10 working days, covering mechanical leveling, rail alignment, electrical hookup, safety zone programming, and operator training.
Q: What electrical power supply is required for standard configurations?
A: The system operates on 380V-480V AC, 3-phase, 50/60 Hz supply. Total power consumption ranges between 25 kVA and 65 kVA depending on the integrated welding power source capacity.
Hot Tags: gantry welding robot for large workpieces, China gantry welding robot for large workpieces manufacturers, suppliers, factory, Argon Arc Welding Robot, cobot robot welding cobot, Collaborative TIG Welding Robot, robotic arc welding cell, robotic welding fabrication system, welding robot transfer workstation system